Forecast the accepted grade rather than generic PAM
A repeat polyacrylamide flocculant requirement should identify each accepted code and the process that uses it. If different grades serve clarification and dewatering, maintain separate stock and consumption records. One aggregate inventory figure can hide a shortage of the material needed by a critical machine.
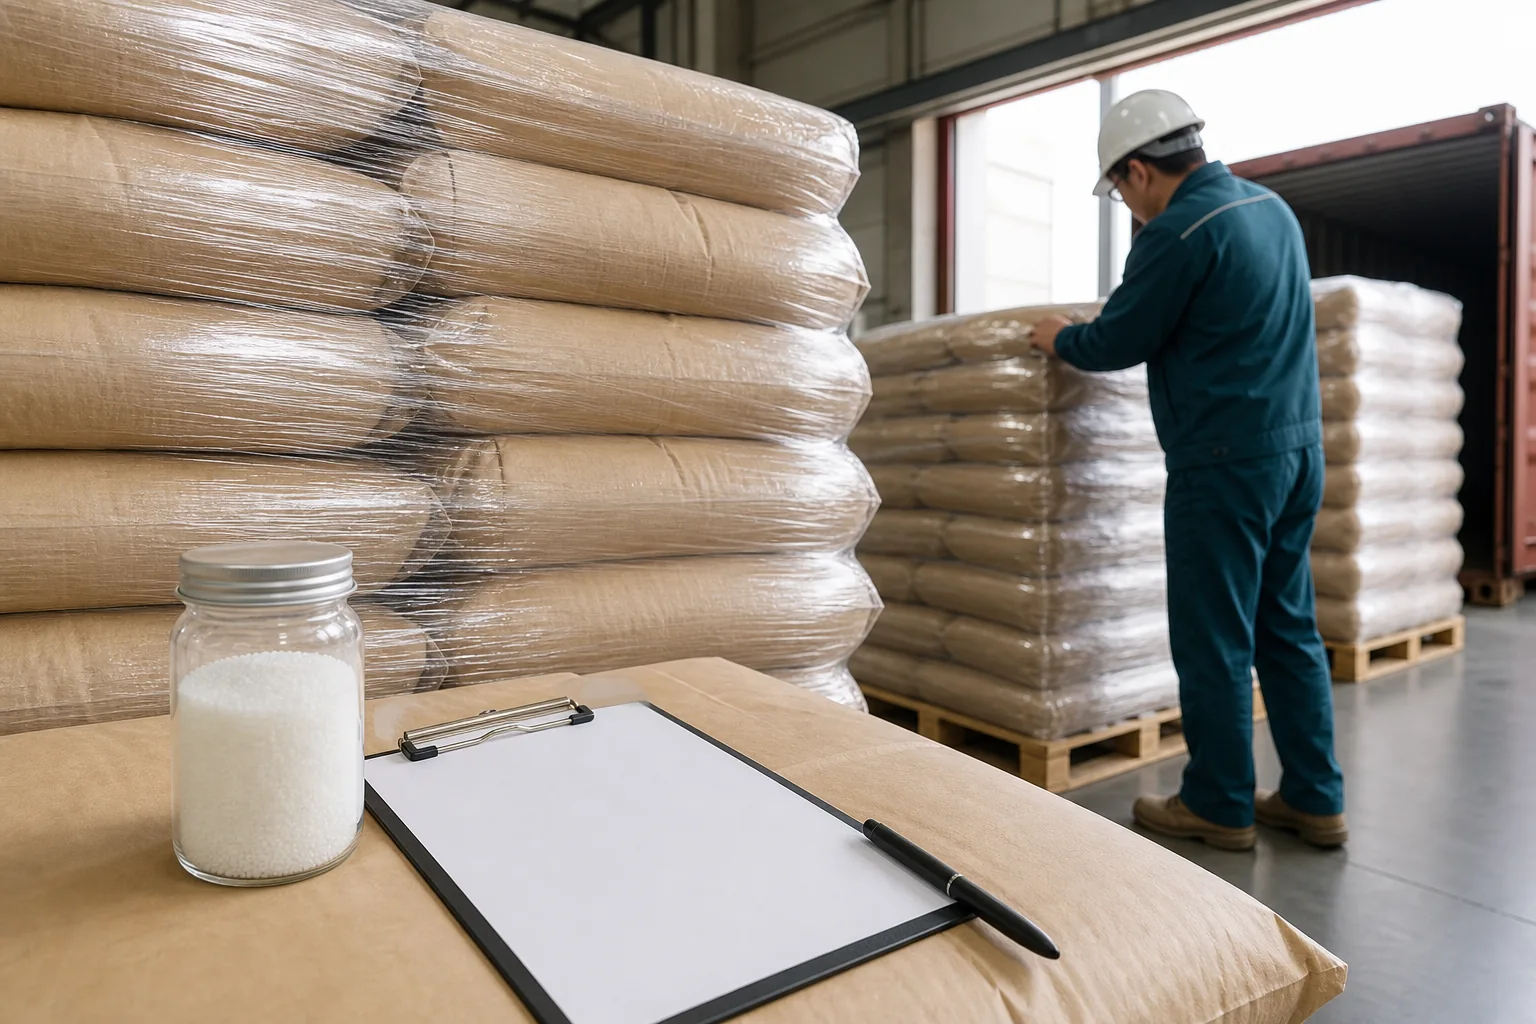
Count usable accepted stock and separate held, unidentified or damaged packages. Convert package counts into mass using the actual agreed net content. Keep the forecast linked to the product and receiving record so material awaiting review is not treated as available supply.
Use current consumption and the actual schedule
Calculate demand from measured use over representative operation and expected plant days or throughput. Review unusual shifts instead of incorporating every spike into the routine baseline. Feed changes, dosing errors or preparation faults can alter consumption without establishing a lasting increase in chemical demand.
For illustration, an assumed 20 kilograms per operating day over 18 operating days requires 360 kilograms before a separately justified reserve. This is arithmetic for planning, not a plant dose recommendation. Replace the inputs with your own records and state how changes in production are reflected in the forecast.
Confirm replenishment assumptions with the supplier
Ask for current availability, order-processing timing and delivery arrangements for the accepted grade, quantity and destination. Include internal approval and receiving time in the plan. A previous delivery is useful experience, but it does not guarantee that every future order follows the same timetable.
Discuss the requirement with Xinqi Polymer supply staff and keep an agreed contact route for changes. The PAM purchasing reference provides context for stock and delivery questions. Commercial commitments should come from the actual order or supply arrangement rather than generic website wording.
Balance reserve with storage and change exposure
A reserve may support continuity, but excess material takes space and can remain unused when an approved grade or process changes. Follow product-specific storage guidance and realistic use periods. Do not increase stock beyond practical handling limits merely to hide an uncertain lead-time assumption.
If a substitute is proposed during a shortage, review its identity, preparation and performance before acceptance. A similar nominal specification does not establish an interchangeable product. Keep the sample-to-order approval chain available when another code needs evaluation.
Define how changes will be recorded
Maintain the accepted grade, packaging, documents and contact responsibilities in the purchasing record. Ask how a proposed product or package change will be communicated and who at the plant will review it. Record revised timing or quantity when a delivery plan changes so operators work from the current information.
The RFQ checklist connects the forecast to an identifiable order. Review consumption, stock and process changes regularly with operations and purchasing together. Reliable repeat supply comes from a maintained material and delivery record, not from an assumed fixed number of bags or an unsupported promise that any PAM grade can cover an emergency.
Review apparently healthy stock with the wrong grade
Suppose the warehouse has substantial PAM inventory but most of it serves another treatment stage. Separate the codes before calculating the remaining operating period. Only accepted usable material for the relevant duty belongs in that duty’s stock balance; a total polymer tonnage can give purchasing a false sense of continuity.
Confirm current consumption and replenishment timing for the shortage-prone code. If an alternative is proposed, keep it subject to the technical approval process rather than using inventory pressure as proof of suitability. The revised plan should identify who reviews the forecast and how a change of process, delivery or product will reach operators before the next run.
| Review point | Evidence to retain |
|---|---|
| Stock | Usable inventory counted by approved code |
| Timing | Current lead-time assumption confirmed |
| Changes | Owner for substitution and forecast review |